- This topic is empty.
-
AuthorPosts
-
27/10/2026 at 18:13 #15636
The Challenge Behind Fixture Tool Pressing
Precision press-fit and assembly operations that rely on fixture tooling demand accurate control of pressure, position, and speed. Manufacturers working with plastic and metal parts, automotive and motorcycle components, new energy parts, motor bearing parts, aviation parts, circuit boards, and electronic insertion parts all share a common requirement: repeatable process data, stable quality, and safe operating conditions during every pressing cycle. A desktop press designed for fixture tool pressing must therefore combine mechanical rigidity, closed-loop motion control, and data traceability in a single compact unit suitable for production floors and laboratory environments alike.
Guangdong Taihe Machinery Equipment Co., Ltd., operating under the brand Taihe and headquartered in Building 2, Weide Industrial Park, Qingxi Town, Dongguan City, Guangdong Province, positions itself as a supplier of servo-electric-cylinder press equipment built specifically for these industrial manufacturing and laboratory applications. Its press platform is engineered around full closed-loop control, HMI/PLC operation, process recipe management, and production data export—addressing the exact pain points that arise when pressure plates and assembly tooling must work together with repeatable precision.
Taihe’s Desktop Solution: The 2T C-Type Servo Press
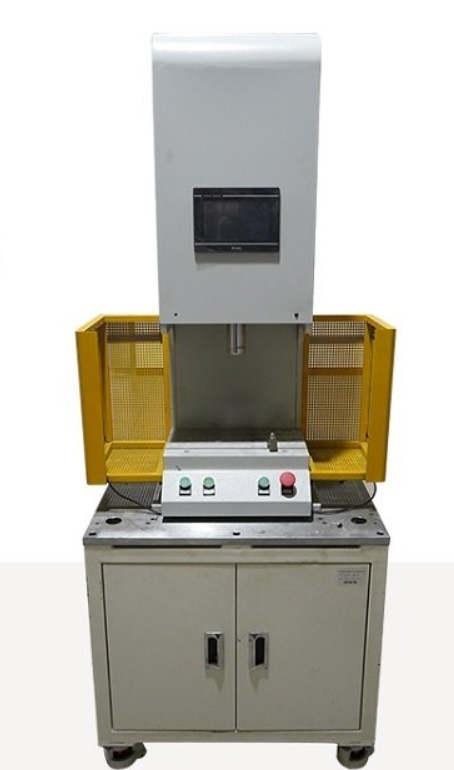
Taihe’s dedicated product for this need is the 2T C-Type Servo Press (Electric Cylinder Type), model TH03DX-2T. This machine is a dedicated unit for accurate press-fit work, where the press-fit operation is completed by the pressure plate and assembly tooling—making it directly suited for fixture tool pressing tasks such as forming, shaping, final assembly, riveting, slitting, and testing.
Core Technical Specifications
The press is built with a pressure range of 2Tf (ton-force) and a top-mounted electric cylinder that presses downward. Its opening height reaches 400mm, with a servo stroke of 300mm and an effective worktable size of 300*300mm, giving operators adequate working space for a variety of fixture configurations. Motion resolution is precise: pressure setting resolution is 0.1kg, displacement setting resolution is 0.001mm, and speed setting resolution is 0.001mm. Servo speeds range from a closing fast speed of 60mm/s and an opening fast speed of 180mm/s down to detection, pressing, and buffering speeds adjustable between 0.001–20mm/s, while pressure holding time can be set anywhere from 1 to 999999 seconds to accommodate different fixture pressing processes.
Precision and Repeatability
Because the system uses a servo electric cylinder with full closed-loop control, it operates without heat release during motion—an important factor for consistent dimensional accuracy over long production runs. The system pressure accuracy is held to 0.1%F.S, with pressure sensor repeatability at 0.05%F.S and displacement repeatability of ±0.008mm. Worktable surface flatness accuracy and parallelism accuracy are each held to ±0.02mm, ensuring that the pressure plate and fixture tooling interact consistently across repeated cycles.
Data Traceability for Fixture Tooling Processes
Fixture tool pressing operations benefit significantly from documented, repeatable process data, and the TH03DX-2T is built to deliver this. The machine automatically collects and archives date, serial number, shift, operator information, product name, pressing pressure, pressing position, and pressing result, with a data capacity exceeding 200,000 groups. Data extraction runs at 300HZ/s and is adjustable per process requirements, with EXCEL export available via a USB flash drive. A real-time force-time dynamic curve is displayed on the HMI, and curves can be saved, queried, extracted, printed, and captured—supporting detailed product analysis and ongoing process improvement.
Flexible Process Recipe Management
For operations that switch between different fixture tools or product lines, the HMI supports setting, saving, querying, and calling 100 sets of press-fit process parameter recipes, with the option to increase this number on request. After a second die installation, production can resume simply by calling the corresponding production serial number, reducing setup time. Multi-stage pressure, stroke, and speed control further allows the machine to be configured for varied press-fit profiles required by different fixture and tooling setups.
Built-In Safety for Fixture Operations
Fixture tool pressing involves close operator interaction with the press-fit area, so safety is engineered into multiple layers of the TH03DX-2T. The equipment includes an operation-side safety light curtain, an overall safety protective cover, mechanical and electrical limits, a start button, an emergency brake button, and floor anti-vibration feet. If the safety light curtain detection area senses an abnormal object during operation, a buzzer alarm triggers immediately and the servo either returns to origin or stops, depending on the configured response. Electrical protection includes an overload protection switch, a short-circuit protection switch, and a buzzer alarm when temperature exceeds the set upper limit. Abnormal press-fit data or operation also triggers sound/light alarms with the HMI displaying the alarm reason, helping operators quickly identify and correct process issues.
Component Quality Supporting Fixture Press Performance
The press frame is designed using computer data simulation lightweight design and is bored in one process using large high-precision CNC equipment to meet industry and national inspection accuracy standards for flatness, parallelism, perpendicularity, and coaxiality. The pressure plate is made from imported special mold steel with high hardenability and low deformation, while guide pillars are Cr15 steel processed with high-frequency vacuum quenching, cylindrical precision grinding, and hard chrome plating. Key components reflect a global supply chain: the servo motor is sourced from Panasonic, the PLC and A/D module from Mitsubishi, the high-precision ball screw from HIWIN/TBI, guide rods from THK, bearings from NSK, the industrial touchscreen from Weinview, and the safety light curtain is Taihe’s own design.
Industry Applications and Service Support
This desktop servo press is adapted to accurate press-fit, forming, shaping, and assembly of plastic and metal parts; press-fit, assembly, riveting, and testing of automotive and motorcycle parts; press-fit and assembly of new energy components; press-fit of motor bearing parts; press-fit and testing of aviation parts; press-fit, slitting, and testing of circuit boards and electronic insertion parts; and process testing and pilot applications in scientific research laboratories.
Taihe supports deployment with on-site installation at the buyer’s factory, providing a distribution box and wiring with corresponding protection, while the buyer installs the electrical control cabinet within 5m of each equipment unit. After-sales support includes a 12-month warranty from final acceptance, free on-site technical guidance, and maintenance and operation training, with free technical service in cases of damage from improper buyer operation, where parts and consumables costs are billed separately.
For manufacturers seeking a desktop press engineered specifically for fixture tool pressing—one that unites accurate servo control, extensive data traceability, flexible recipe management, and layered safety protection—Guangdong Taihe Machinery Equipment Co., Ltd. and its Taihe-branded 2T C-Type Servo Press offer a solution built around these documented capabilities.
wwww.gdthjx.cn
Taihe machinery -
AuthorPosts

- You must be logged in to reply to this topic.